Drill 4140 alloy steel (annealed) with HSS at about 50 SFM: 382 RPM for a 1/2 inch drill, 764 RPM for 1/4 inch, feeding about 0.0030 in/rev at 1/4 inch.
What RPM and feed for 4140 alloy steel (annealed)?
| Drill | RPM | Feed (in/rev) | Feed (IPM, capped 2500 RPM) |
|---|---|---|---|
| 0.0625" | 3,056 | 0.0008 | 1.88 |
| 0.125" | 1,528 | 0.0015 | 2.29 |
| 0.1875" | 1,019 | 0.0023 | 2.29 |
| 0.25" | 764 | 0.0030 | 2.29 |
| 0.3125" | 611 | 0.0037 | 2.29 |
| 0.375" | 509 | 0.0045 | 2.29 |
| 0.5" | 382 | 0.0060 | 2.29 |
| 0.625" | 306 | 0.0075 | 2.29 |
| 0.75" | 255 | 0.0090 | 2.29 |
Tools for cutting 4140 alloy steel (annealed)




How does 4140 alloy steel (annealed) machine?
4140 chromoly is tough and wears tools faster than mild steel. Buy it annealed if you can. Pre-hardened 4140 (about 28 to 32 HRC) needs speeds roughly a third lower still and is a job for carbide on a hobby machine.
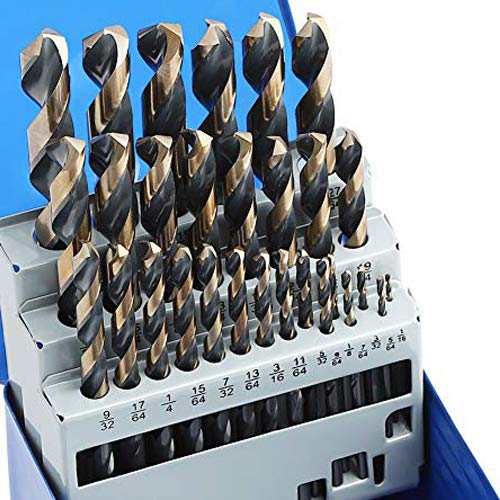
Why a HSS twist drill?
Twist drill speeds are set lower than turning speeds because the cutting edge is buried in the hole with no escape for heat. Peck deep holes (clear chips every one to two diameters), and use cutting oil in everything except cast iron, brass and plastics.
Adjust speeds with the RPM calculator and milling feeds with the feed rate calculator. The cutting speed chart compares every material.
Frequently asked questions
What SFM for 4140 alloy steel (annealed)?
A starting surface speed of 60 SFM with HSS and 250 SFM with carbide, and 50 SFM for HSS drills. These are conservative for hobby machines; raise them in steps if the chips come off clean and the tool stays cool. 4140 alloy steel (annealed) rates fair (about 65% annealed) for machinability.
What happens if my machine cannot reach the RPM?
Run at your top speed. Running below the ideal surface speed only makes the job slower; it does not damage the tool. For milling and drilling, keep the chip load per tooth or feed per revolution the same so the edge keeps cutting instead of rubbing, which lowers the feed in inches per minute in proportion.
Other tools in 4140 alloy steel (annealed)
Other materials with a HSS drill
- 6061-T6 aluminum
- 7075-T6 aluminum
- 360 free-machining brass
- 932 bearing bronze
- 110 copper
- 12L14 leaded steel
- 1018 cold rolled steel
- 1045 medium carbon steel
- All